

RúllumótunarlínaLinia CZS
Zeman




Grunnupplýsingar
- Heiti vélar:
- Rúllumótunarlína
- Framleiðandi:
- Linia CZS
- Gerð:
- Zeman
- Framleiðsluár:
- 2010
- Ástand:
- næstum eins og nýtt (notað)
- Virkni:
- fullkomlega virkur
Verð og staðsetning
- Staðsetning:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
Tilboðsupplýsingar
- Auglýsingarauðkenni:
- A21299532
- Uppfærsla:
- síðast þann 22.07.2026
Lýsing
ZEMAN CZS LINE SPECIFICATIONS
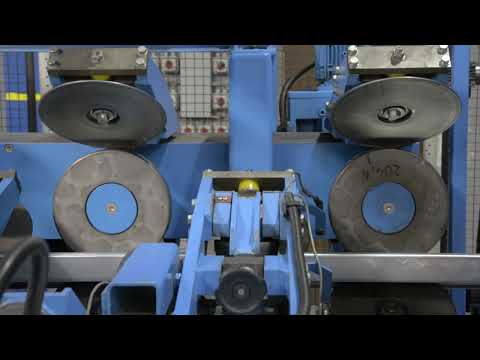
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
Dkedeymampopfx Agvou
6. Rotary Cut-Off Guillotine.
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
Bjóðandi
Síðast á netinu: Í gær
Skráð frá: 2006
188 Auglýsingar á netinu

Senda fyrirspurn
Sími & Fax


 Þýskaland
SpinnerTC 65-MC


 Beograd
GaspariniSlitter


 Eschborn
Deckel MahoDMF 250 linear


 Reiden
GoodwayGS-2800 M


 Weilerswist
TEMAREDCar Flat 3518 für PKW bis 1.438 kg - Kippbar


 Þýskaland
GildemeisterCTX 200E


 Wolfern
ProthPSGC-50120AHR NEUER PREIS!


 Blumberg
HWACHEONCutex 160 B


 Þýskaland
SpinnerVC 750

 Fevziçakmak
TFON MACHINE CO.Leveling Machine | TF-L 9016

Machineseeker-traustmerki
Hvað er traustvottorð?
Machineseeker vottar valda söluaðila með traustsvottun Machineseeker. Áður en úthlutað er framkvæma reyndir starfsmenn Machineseeker staðlaða og yfirgripsmikla skoðun.
Hvað skoðum við?

Staðfesting á
rekstrarleyfi eða útdrætti úr firmaskrá
Yfirferð á
póstfangi seljanda
Staðfesting á
bankatengingu
Staðfesting á
símalegu
aðgengi að aðalnúmerinu
Efnahagsupplýsingar
mega ekki innihalda neikvæða eiginleika
Kaupendur kvartanir
geta leitt til þess að vottunin verði afturkölluðHvað þýðir þetta fyrir þig sem kaupanda?
Með Machineseeker-traustmerkinu getur þú sem kaupandi þekkt áreiðanlega seljendur, jafnvel án eigin athugunar, sem líklega stunda heiðarlega og réttláta viðskiptahætti.
Auðvitað geta samt sem áður orðið ágreiningar á meðan á kaupferlinu stendur. Machineseeker ber ekki ábyrgð á brotum á lögum sem virkir kaupendur eða seljendur á Machineseeker kunna að fremja.